Diamond rotary dressing rolls,
made to your drawing.
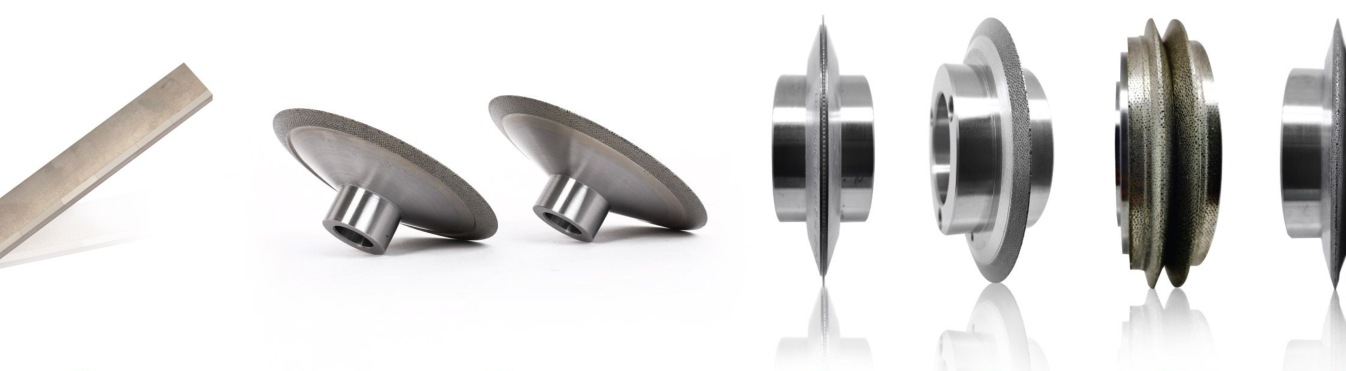
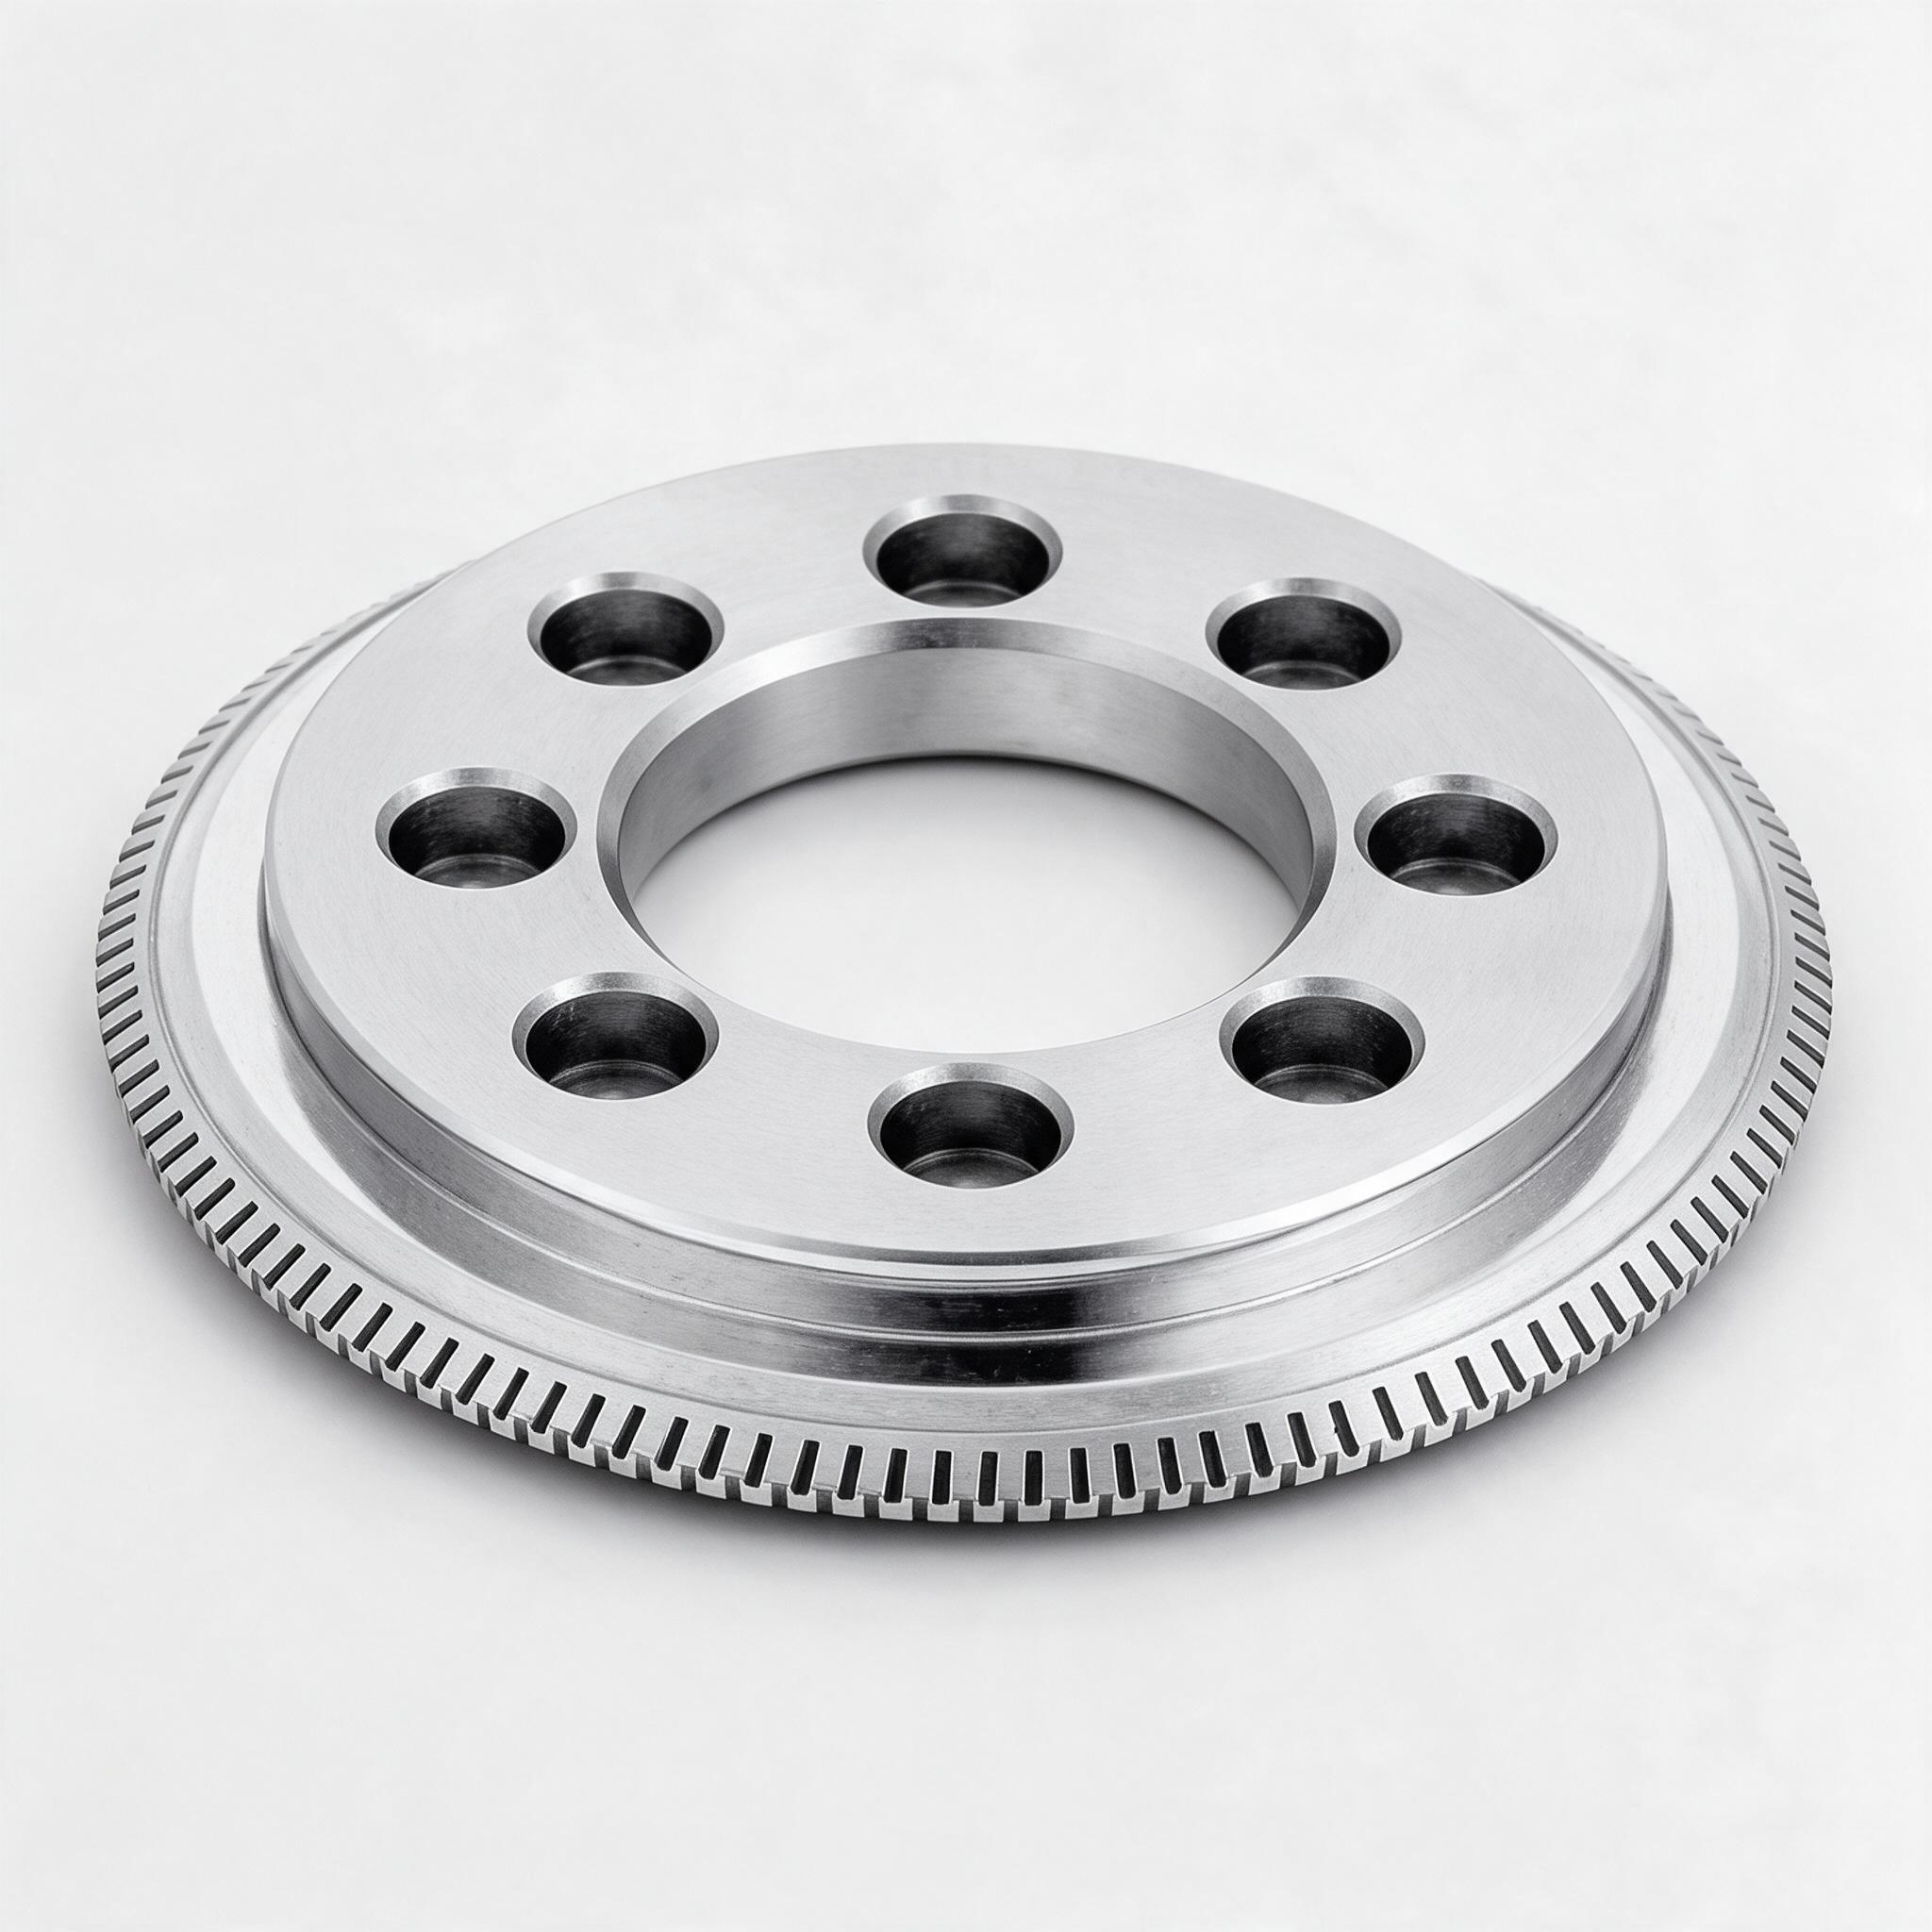
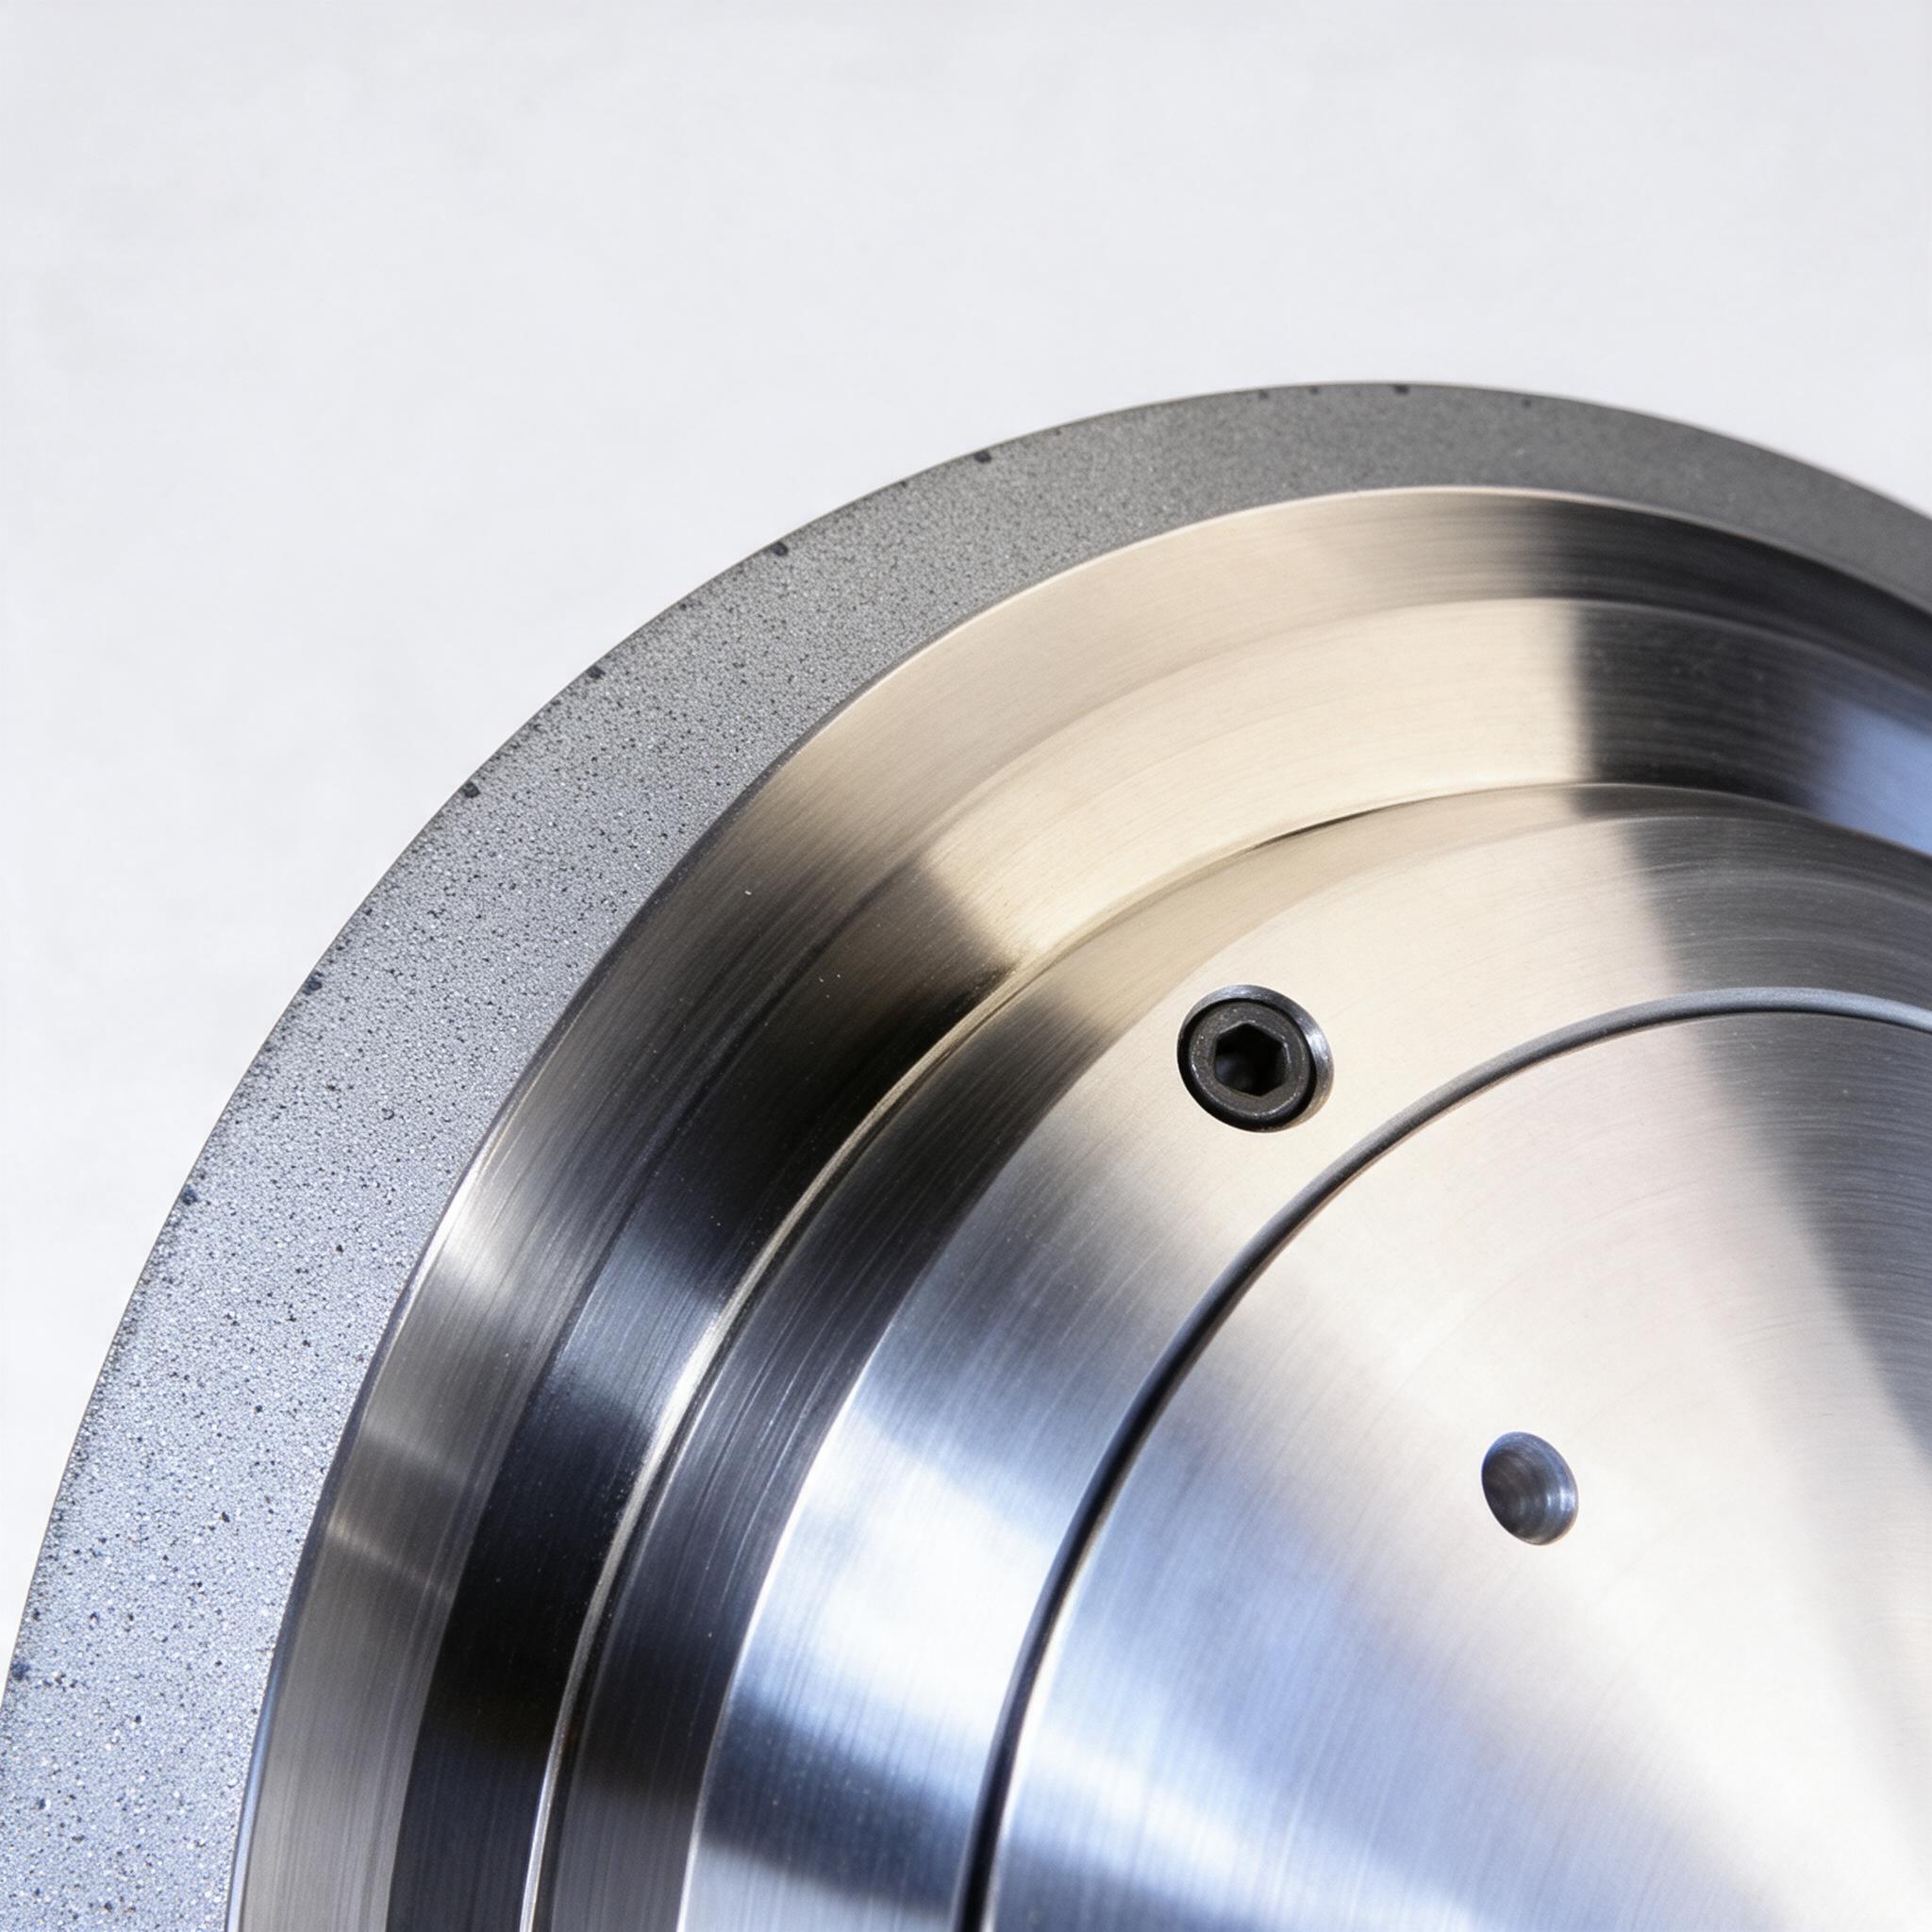
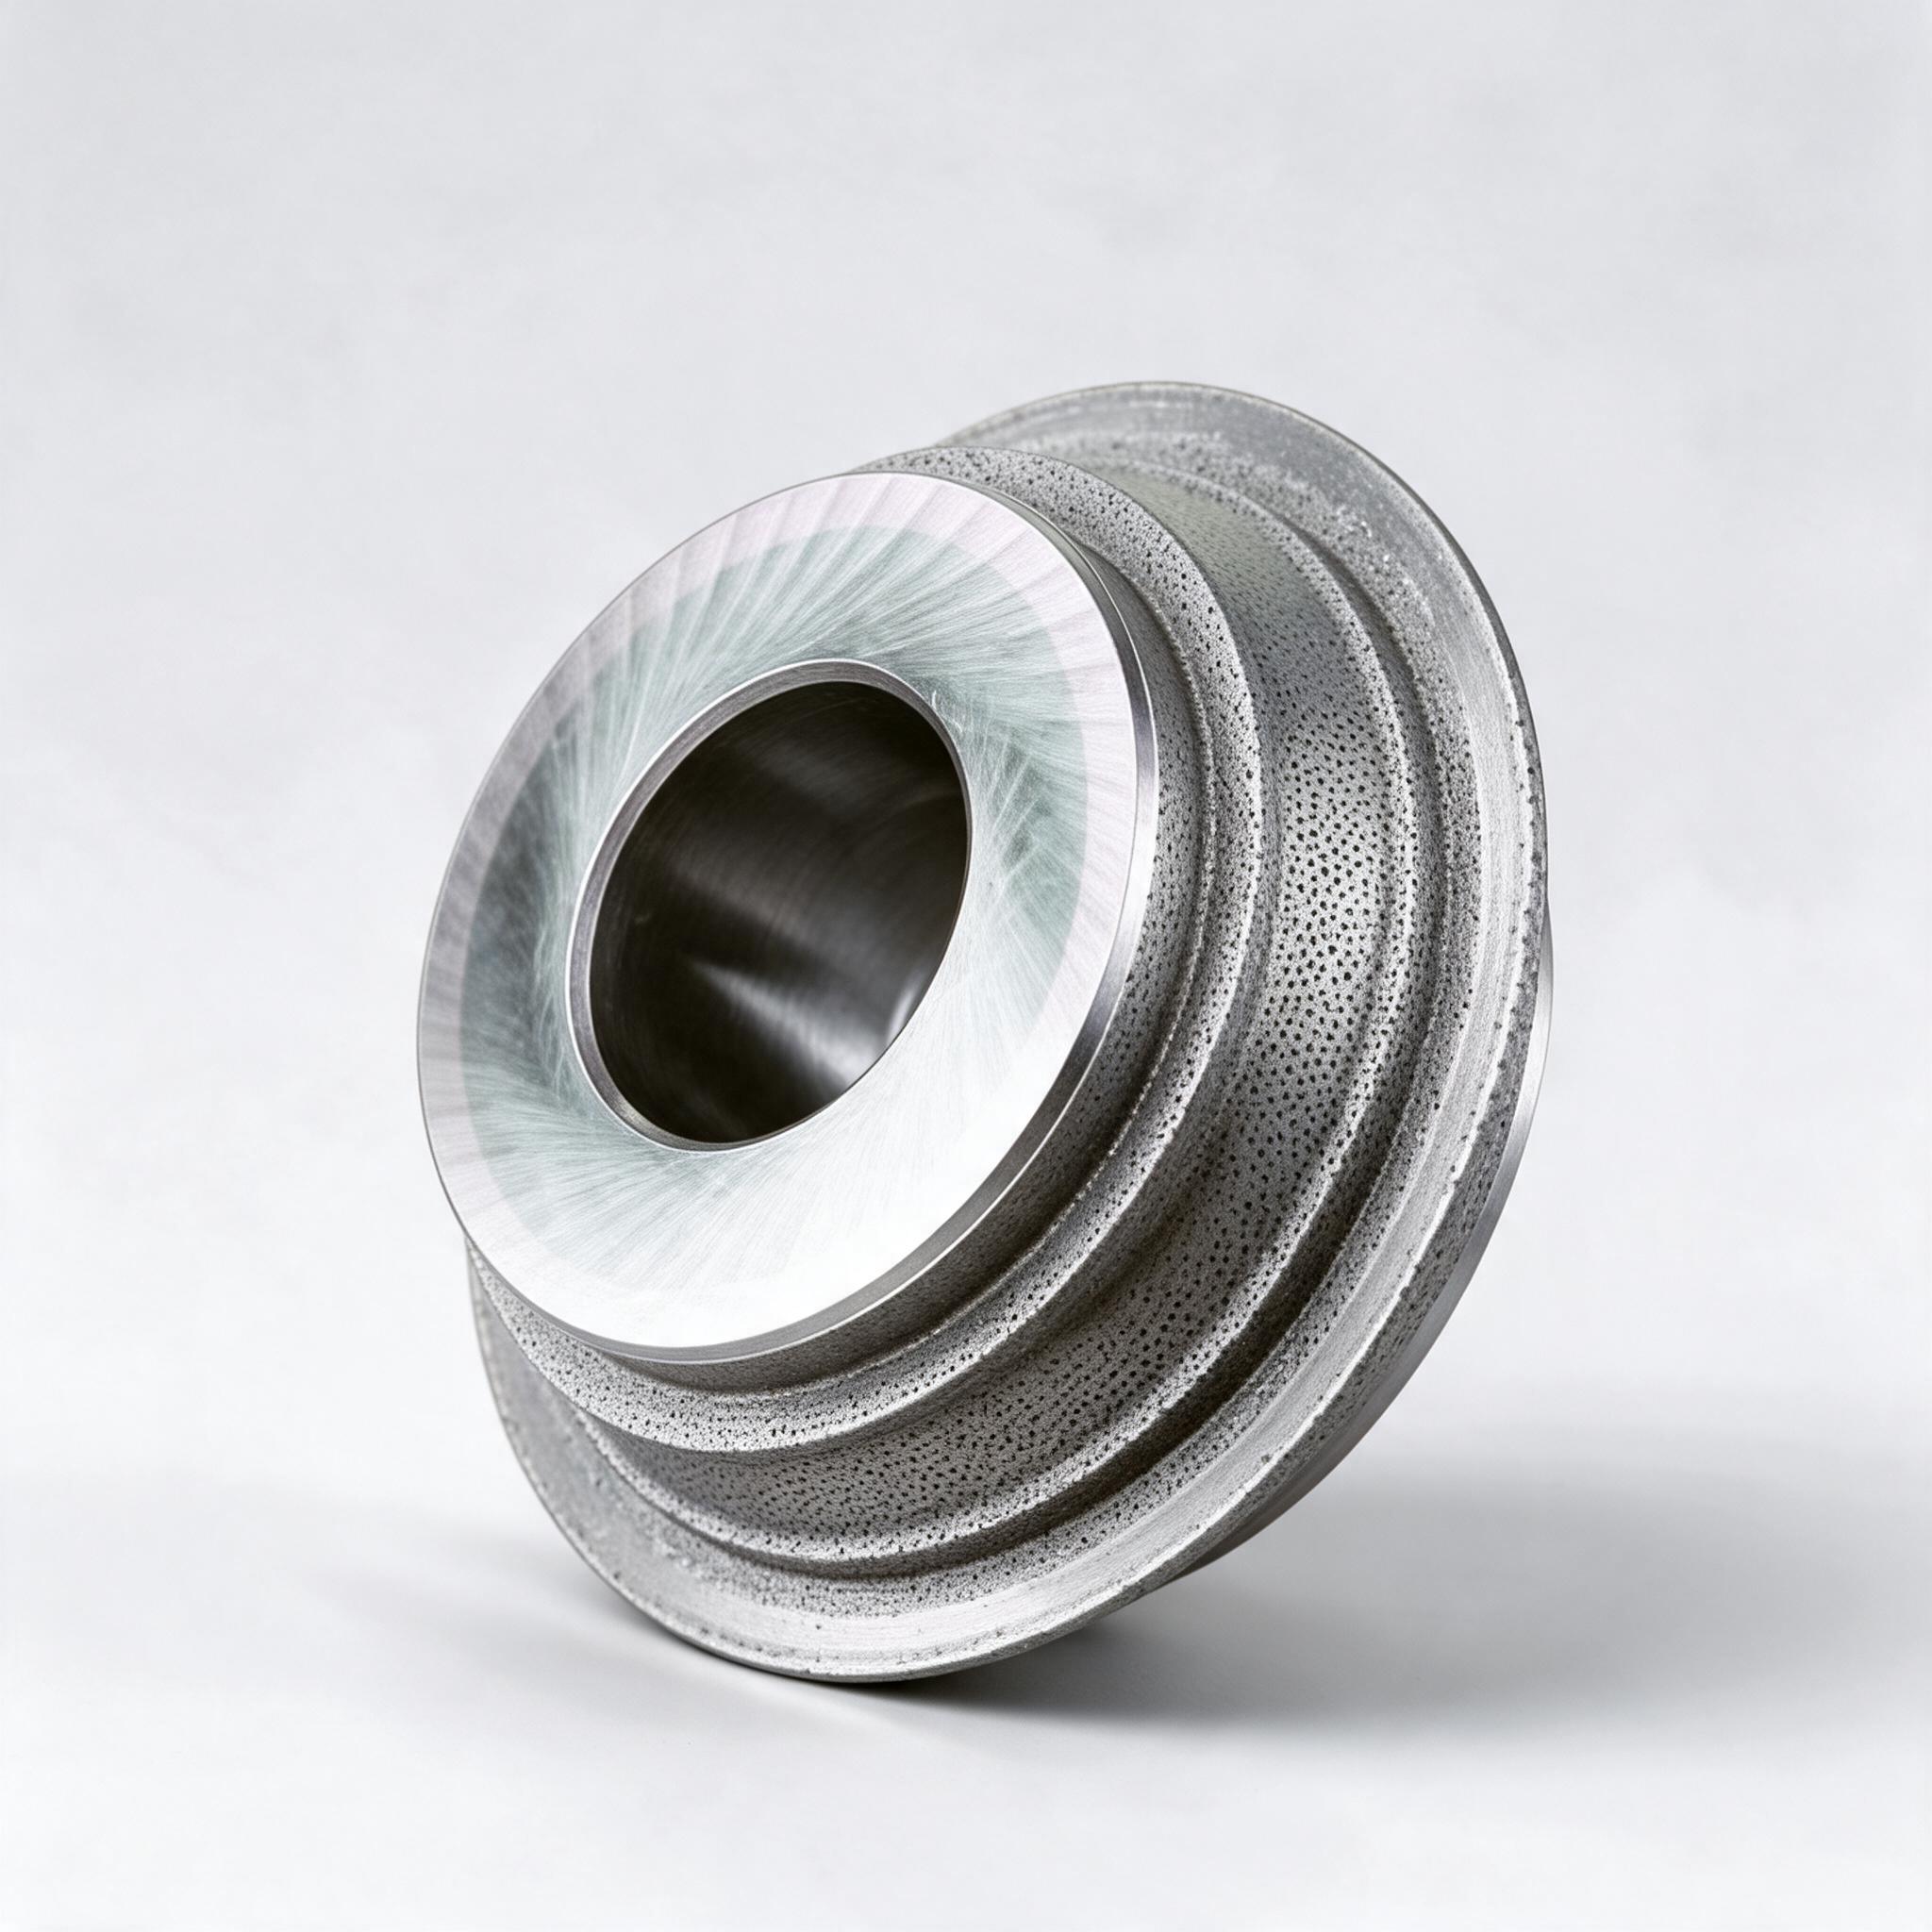
We make the rolls that keep vitrified grinding wheels true — single-cone, double-plate, form and worm-grinding combination rolls. Supplied to gear, bearing and precision grinding shops, with a profile report for every batch.
About SEAJON
A specialist in precision superabrasive tools
Shanghai Xinjian Machinery was founded in 2012 in Minhang District, Shanghai. We focus on supplying high-end precision abrasive products and on full-chain support for imported precision grinding machines. Over more than a decade we have stayed in one narrow lane, building deep selection know-how, a responsive supply chain and application-level technical support. That focus has made us a long-term partner to high-end manufacturers across the Yangtze River Delta and the rest of China.
From the start we took a deliberately different position: put more than ten years of industry resources into high-precision grinding, and nothing else. More than 75% of our products are customized to a customer's specific machining requirement, including ultra-high-precision profiles that ordinary suppliers decline. Our products and services now reach aerospace structural parts, automotive core components, high-precision bearings, gear grinding, technical ceramics, semiconductor SiC wafer processing, precision tool grinding and dozens of other demanding sectors. More than 60% of our customers have stayed with us since our early years, and both repeat-purchase and referral rates remain at the top of our niche.
Our core team brings more than ten years of abrasive-tool technical service experience, and supports customers from product selection through to later process optimization. We work by a simple principle — integrity first, service first, simplicity, and respect for the customer — and we look forward to long-term technical partnerships with manufacturers who need to solve the hardest grinding problems.
Over ten years of vertical focus on precision grinding consumables.
More than 75% of our output is customized to the customer's own specification.
Over 60% of our customers have stayed with us since the early years.
Quality management certified, with a full import & export licence.
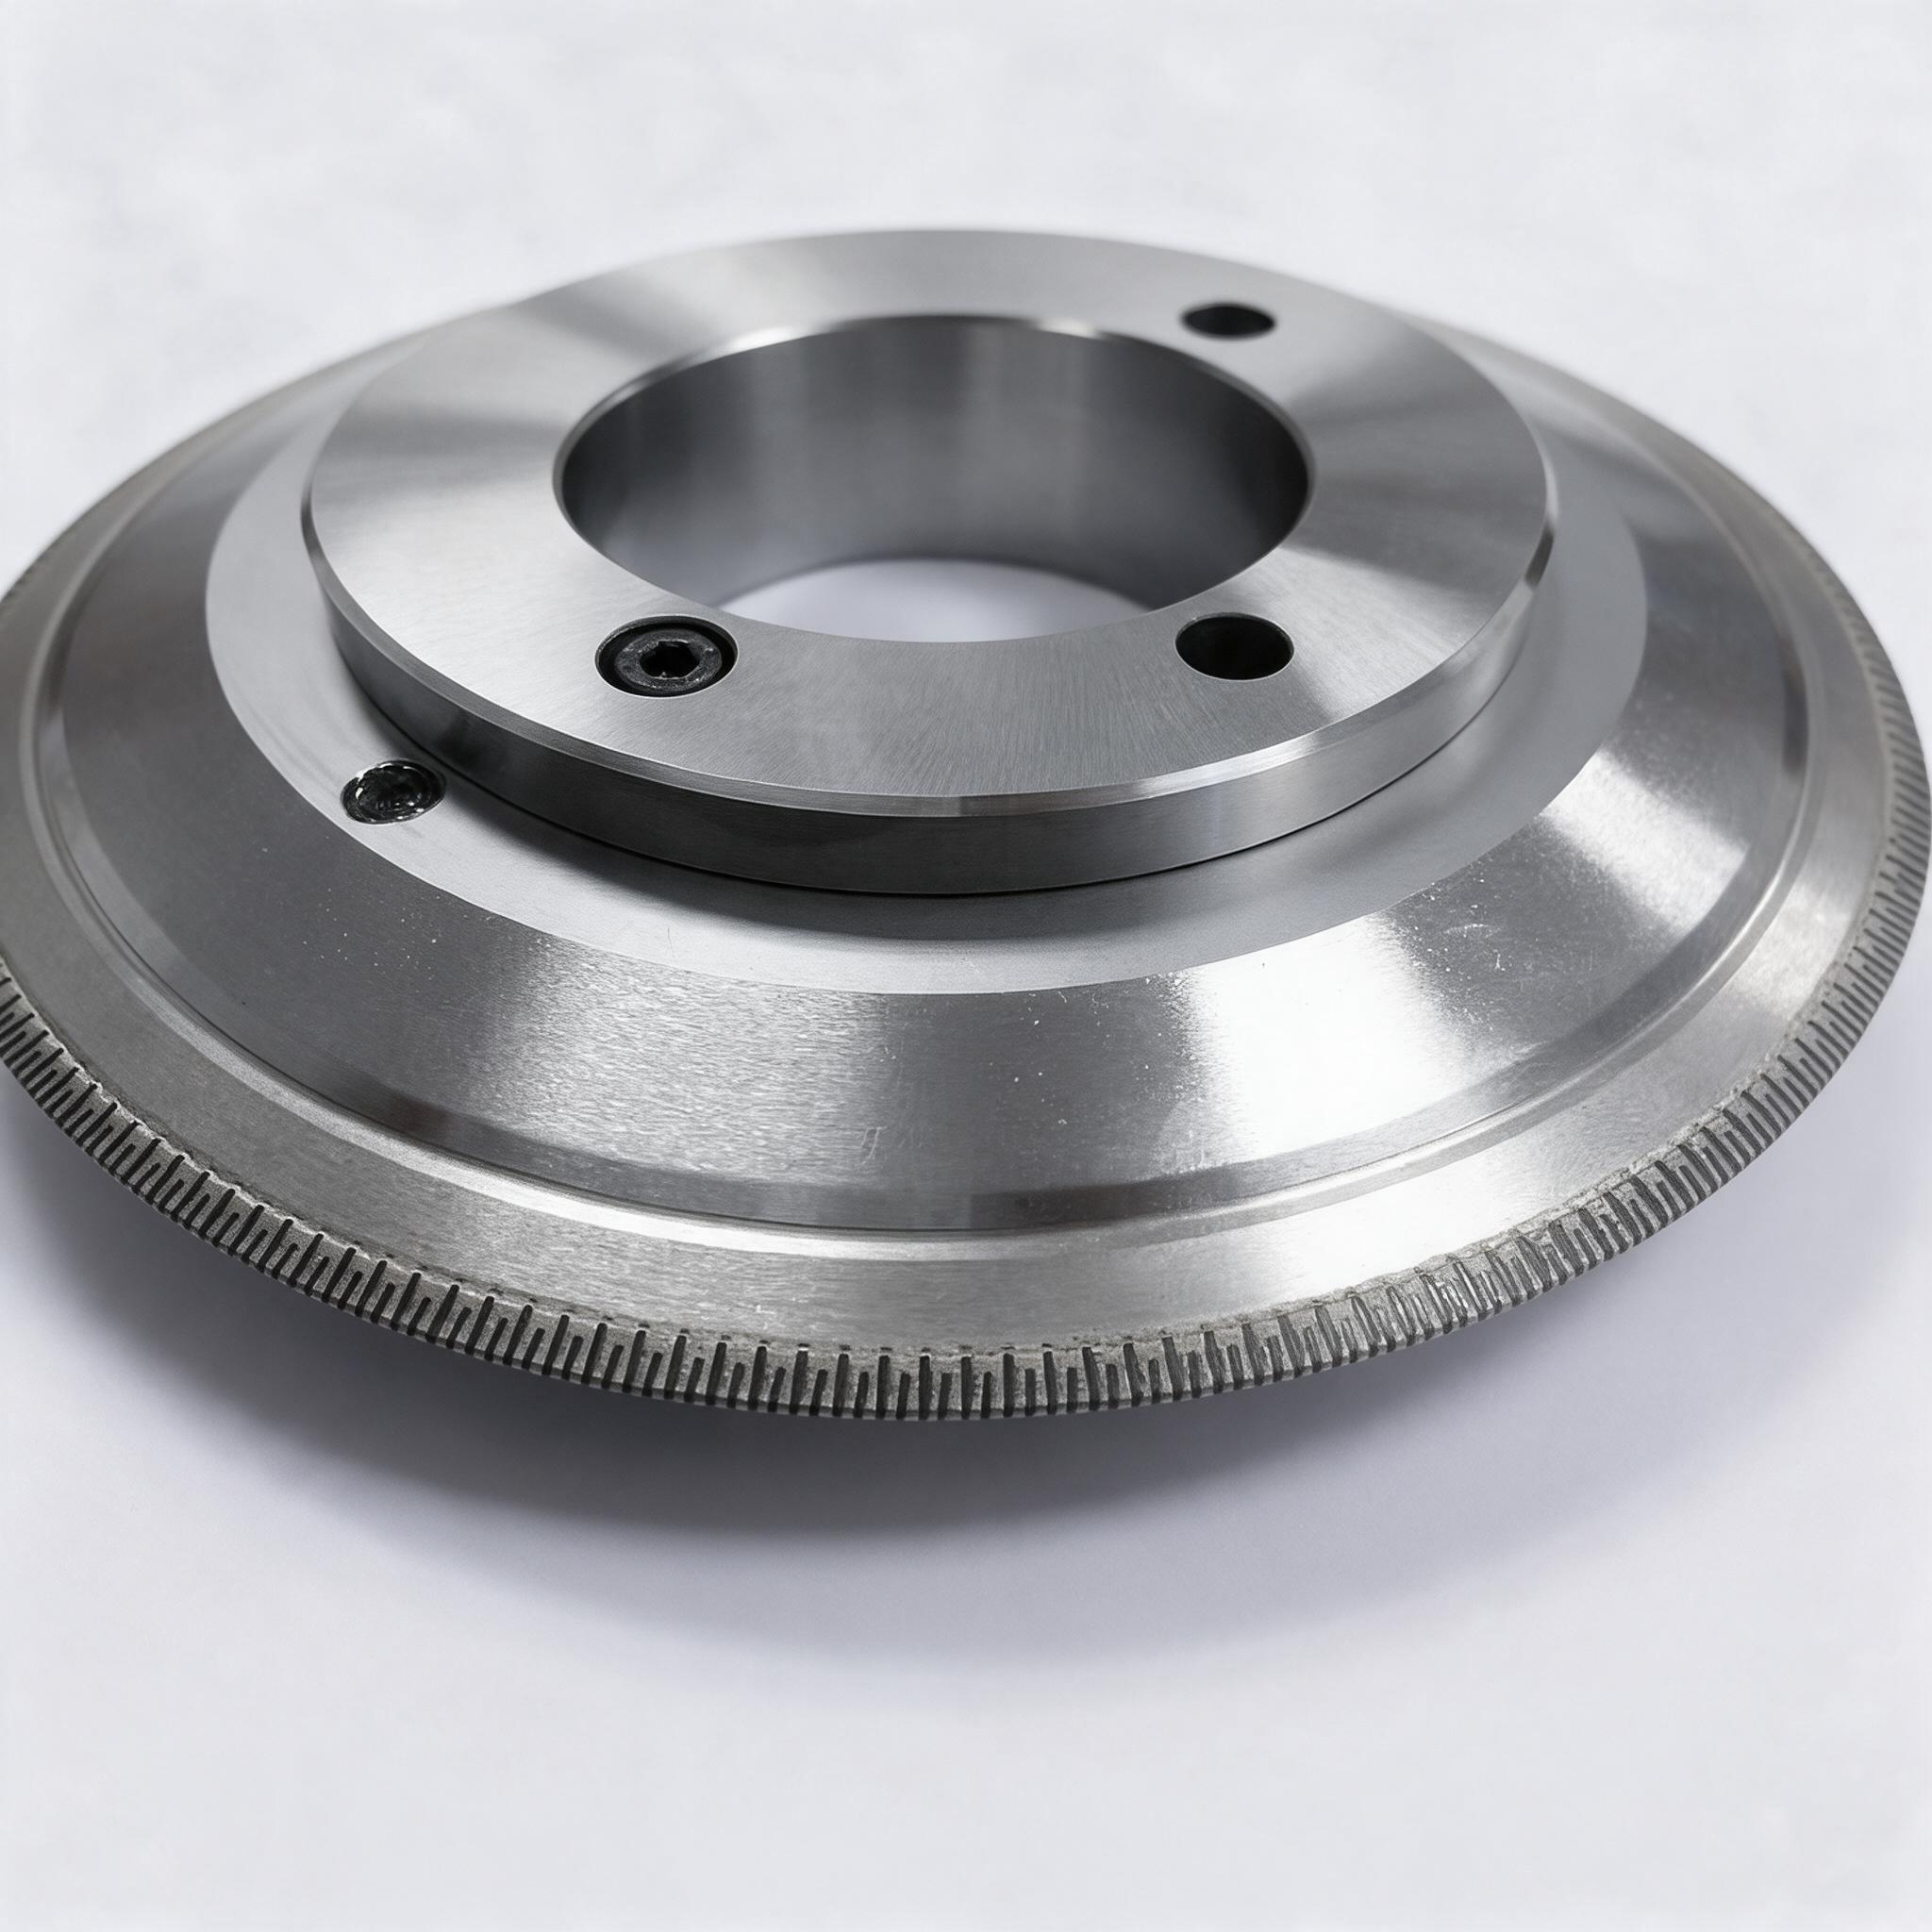
- Aerospace precision structures and engine components
- Automotive powertrain and core components
- High-precision bearings and gear manufacturing
- Cutting tools, technical ceramics and semiconductor SiC wafers
- Steel and general precision machining
Product range
Every dressing position on the wheel
Produced to your drawing, not from a fixed catalogue. If you send a worn roll, we measure it and quote against the measured profile.
Single-cone & combination rolls
Straight and angle dressing on cylindrical and surface grinders.
- Multi-step forms in one roll
- Bore and mounting to your spindle
- Used where one roll dresses several wheel faces
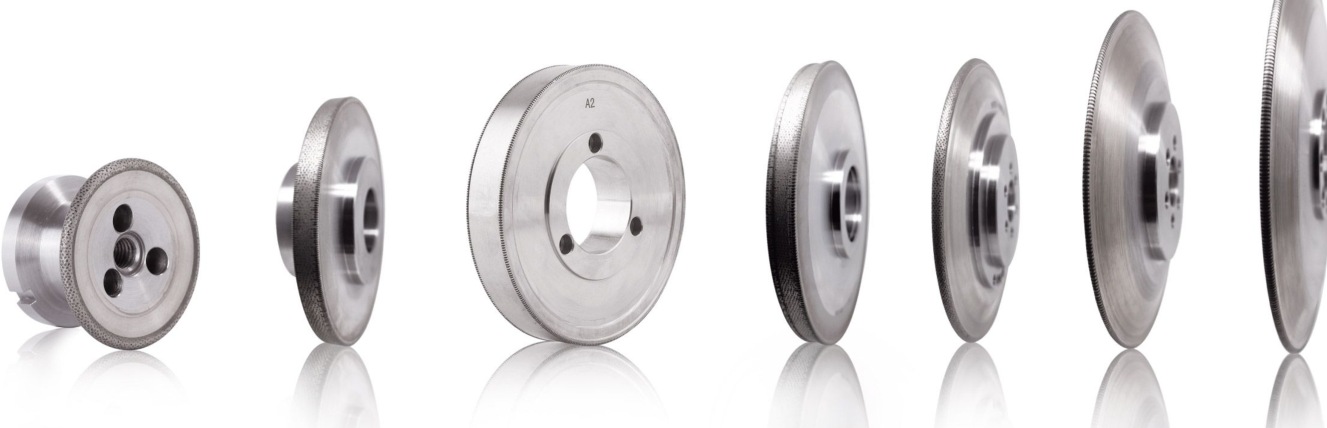
Double-plate & universal rolls
Two diamond layers for long runs between replating.
- Longer intervals between replacement
- Higher form stability at high volume
- Universal body for several wheel profiles
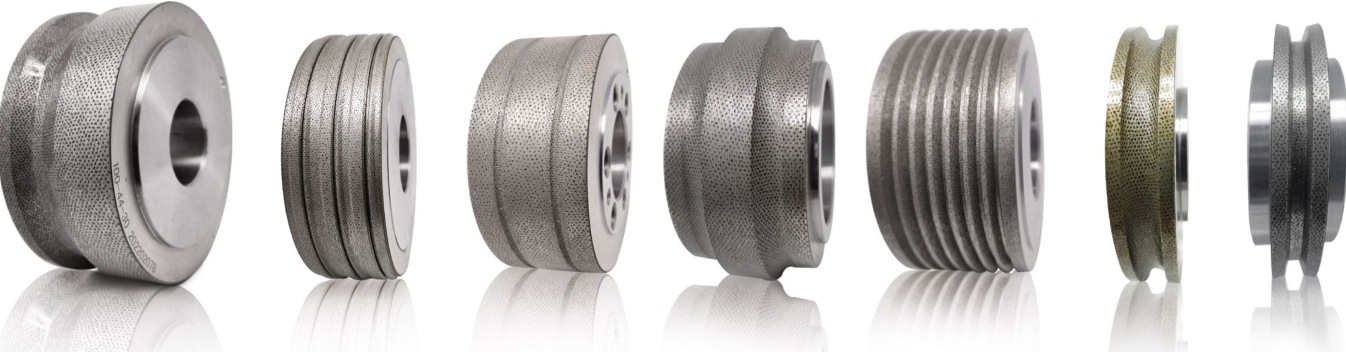
Profile form rolls
Full-profile rolls for gear and rack grinding.
- Involute and non-involute profiles
- Single and multi-start forms
- Profile trace supplied with each batch
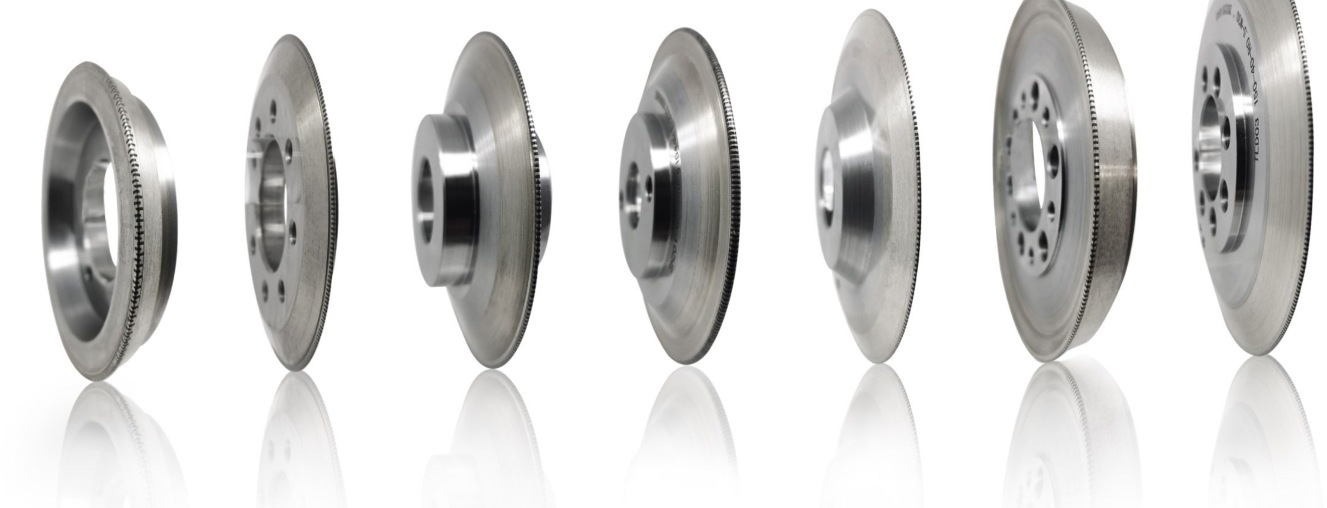
Worm-grinding rolls & CVD disc dressers
For continuous generating grinding and fine wheel finishing.
- Combination rolls for worm grinding
- CVD disc dressers for the wheel face
- Matched to KAPP, NILES, Reishauer geometry
Technical data
Typical range
Indicative values. Everything is confirmed against your drawing before quotation — we do not force a size that does not suit your machine.
| Outer diameter | 50–400 mm (larger on request) |
|---|---|
| Bore / mounting | To drawing; H6 typical |
| Diamond layer | Single or double |
| Diamond grit | D64–D181 (approx. 230/270–80/100 mesh) |
| Profile tolerance | ±0.01 mm typical; ±0.005 mm on request |
| Max profile depth | Up to 30 mm |
| Wheel bond | Vitrified (ceramic); resin on request |
| Body | Hardened steel, to drawing |
| Replating | 2–3 cycles depending on body condition |
Applications
Where a dressing roll pays for itself
Any operation running ceramic-bond wheels in volume, with a profile that has to hold from the first part to the last. Single-piece work is usually better served by a hand dresser.
Capability
What we commit to
Four commitments we can hold, rather than ten we cannot.
Your profile, grade, bore and mounting. No forced catalogue sizes.
Measured profile and runout record with every lot.
Against 60+ days from most original equipment suppliers.
Worn rolls stripped and recoated, typically 35–50% of a new roll.
- Measured profile trace with tolerance band
- Runout record on the bore and the dressing face
- Photograph of the diamond layer before packing
- Batch number on the roll and on the packing list
How an order runs
2D drawing, STEP file, or the roll itself. Machine and wheel details help us match the grade.
Price, recommended grade and lead time. We flag anything in the drawing that will not hold in production.
Start with 1–3 rolls, run them on your machine, then move to scheduled batches.
Questions
Before you write
What is the minimum order?
One piece for a trial. There is no minimum on repeat orders.
How long is delivery?
Trial rolls 25–35 days; repeat orders 30–45 days. Expedited production is possible on request.
How do I send a drawing?
PDF, STEP or DWG by email, or send the worn roll itself. If you need an NDA first, say so in your first email.
Can you make a roll for a machine you have never seen?
Yes. We need the drawing or the worn roll, the machine model and the wheel specification.
What are your payment terms?
Typical terms are a deposit with the balance before shipment; letter of credit for larger orders. Confirmed at quotation.
Can you replate our existing rolls?
Yes, if the steel body is sound. Send photos of the body and the worn layer and we will assess it.
How are rolls packed?
Individually protected, rust-prevented, in a wooden case with the packing list and inspection record.
Do you supply anything besides dressing rolls?
Dressing rolls are our core production. For related consumables — brake pad chamfering wheels, special abrasive wheels — we can supply through partner factories where the volume justifies it. Send the machine model and the specification and we will come back with a route.
Contact
Send a drawing, get a price
Tell us the machine, the wheel and what the form has to hold. A photo and a few dimensions of a worn roll are enough to start.
Drawings you send are used only to quote and manufacture your order. We do not resell customer profiles. If you need an NDA before sending a drawing, say so in the first email.